Industrial Efficiency Starts with the Right Conveyor Manufacturer
In today’s competitive industrial landscape, efficiency is no longer optional—it’s a necessity. From manufacturing plants to warehousing and logistics hubs, businesses are constantly looking for ways to streamline operations, reduce downtime, and maximize productivity. One of the most critical yet often overlooked components of this efficiency is the conveyor system. Choosing the right partner among belt conveyor manufacturers in india can significantly influence your operational success.
A well-designed conveyor system not only improves workflow but also ensures safety, consistency, and scalability. This is where experienced manufacturers step in, offering tailored solutions that align with your specific industry needs.
Why Conveyor Systems Are the Backbone of Industrial Efficiency
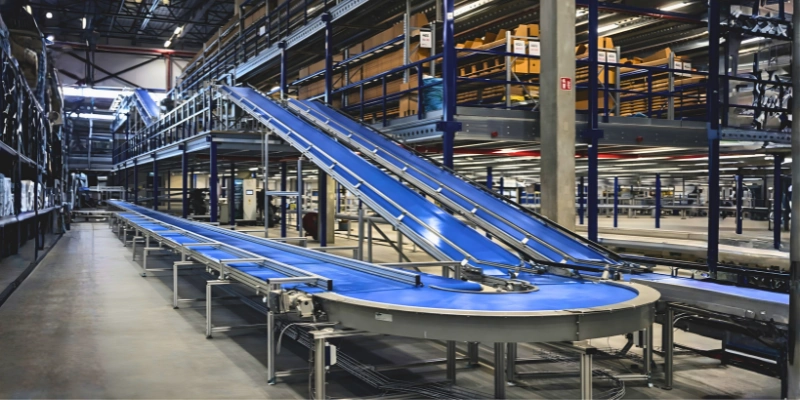
Conveyor systems are more than just material handling tools—they are the lifeline of modern production units. Whether you’re moving raw materials, semi-finished goods, or final products, conveyors enable seamless transportation with minimal human intervention.
Key Benefits of High-Quality Conveyor Systems
- Enhanced Productivity: Automated movement reduces manual labor and speeds up processes.
- Reduced Operational Costs: Lower labor requirements and minimal material wastage.
- Improved Workplace Safety: Controlled material handling reduces accidents.
- Consistent Performance: Ensures uniformity in production cycles.
- Scalability: Easily adaptable to growing business needs.
When sourced from reliable belt conveyor manufacturers in india, these systems become long-term assets that contribute directly to profitability.
Choosing the Right Conveyor Manufacturer
Selecting a conveyor manufacturer is not just about comparing prices—it’s about evaluating expertise, customization capabilities, and long-term support. A trusted manufacturer understands that every industry has unique requirements.
What to Look For in a Manufacturer
1. Industry Experience
A manufacturer with years of experience brings technical knowledge and proven solutions. They can anticipate challenges and offer practical, efficient designs.
2. Customization Capabilities
No two operations are identical. A good manufacturer will design conveyor systems tailored to your workflow, space constraints, and load requirements.
3. Quality Standards
High-quality materials and precision engineering ensure durability and reliability. This reduces maintenance costs and extends the lifespan of the system.
4. After-Sales Support
Timely maintenance and support services are crucial for uninterrupted operations. Reliable manufacturers provide ongoing assistance to keep systems running smoothly.
The Role of Innovation in Conveyor Manufacturing
Modern industries demand more than basic conveyor systems. With advancements in technology, manufacturers are integrating smart features to enhance performance.
Innovations Driving Efficiency
- Automation Integration: Seamless connection with automated production lines.
- Energy-Efficient Designs: Reduced power consumption for sustainable operations.
- Advanced Control Systems: Real-time monitoring and control for better efficiency.
- Durable Materials: مقاistance to wear and tear in harsh environments.
Leading belt conveyor manufacturers in india are continuously evolving to meet these demands, offering solutions that align with Industry 4.0 standards.
Industry Applications of Conveyor Systems
Conveyor systems are widely used across various industries, each requiring specific configurations.
Manufacturing Sector
Used for assembly lines, packaging, and material transport, ensuring smooth production flow.
Warehousing and Logistics
Facilitates efficient sorting, loading, and unloading of goods, improving turnaround time.
Food Processing
Ensures hygienic and safe transportation of food products with specialized conveyor designs.
Mining and Heavy Industries
Handles bulk materials in challenging environments with robust and durable systems.
A reliable manufacturer understands these diverse applications and delivers solutions that meet industry-specific standards.
Why Quality Matters More Than Cost
While cost is an important factor, choosing a conveyor system solely based on price can lead to long-term inefficiencies. Low-quality systems often result in frequent breakdowns, higher maintenance costs, and operational delays.
Long-Term Advantages of Investing in Quality
- Reduced Downtime
- Lower Maintenance Costs
- Higher Productivity
- Improved Safety Standards
- Better Return on Investment (ROI)
Working with established belt conveyor manufacturers in india ensures that you receive a product that delivers consistent performance over time.
How the Right Partner Makes a Difference
A trusted manufacturer does more than just supply equipment—they become a strategic partner in your growth. From initial consultation to installation and maintenance, their expertise ensures that your operations run efficiently.
Companies like Samarth Engineerings focus on delivering solutions that align with modern industrial demands. By understanding client requirements and offering customized systems, they help businesses achieve operational excellence.
When you choose to work with Samarth Engineerings, you’re not just investing in a conveyor system—you’re investing in reliability, innovation, and long-term efficiency.
Steps to Selecting the Ideal Conveyor System
To ensure you make the right choice, follow a structured approach:
Step 1: Assess Your Requirements
Understand your material handling needs, including load type, volume, and distance.
Step 2: Evaluate Space Constraints
Consider the available space and layout of your facility.
Step 3: Define Your Budget
Balance cost with quality to ensure long-term benefits.
Step 4: Consult Experts
Work with experienced manufacturers who can guide you through the selection process.
Step 5: Plan for Future Expansion
Choose systems that can adapt to your business growth.
Common Mistakes to Avoid
Even experienced businesses can make errors when selecting conveyor systems. Avoid these common pitfalls:
- Choosing price over quality
- Ignoring customization needs
- Overlooking maintenance requirements
- Not considering future scalability
- Failing to evaluate manufacturer credibility
By avoiding these mistakes, you can ensure a smooth and efficient operation.
The Future of Conveyor Systems in India
India’s industrial sector is rapidly evolving, driven by automation and technological advancements. Conveyor systems are playing a crucial role in this transformation.
Emerging Trends
- Increased adoption of automated systems
- Focus on energy efficiency and sustainability
- Integration with smart technologies
- Growing demand for customized solutions
As industries continue to expand, the demand for reliable conveyor systems will only increase. Partnering with experienced manufacturers ensures that your business stays ahead of the curve.
Conclusion
Industrial efficiency begins with the right foundation, and conveyor systems are a critical part of that foundation. Choosing the right manufacturer can make all the difference in achieving seamless operations, reducing costs, and improving productivity.
By working with trusted experts and investing in high-quality systems, businesses can unlock new levels of efficiency and growth. Whether you’re upgrading existing systems or setting up a new facility, the right conveyor partner will help you move forward with confidence.
In a world where efficiency defines success, making the right choice today ensures a stronger, more productive tomorrow.